Problem definition
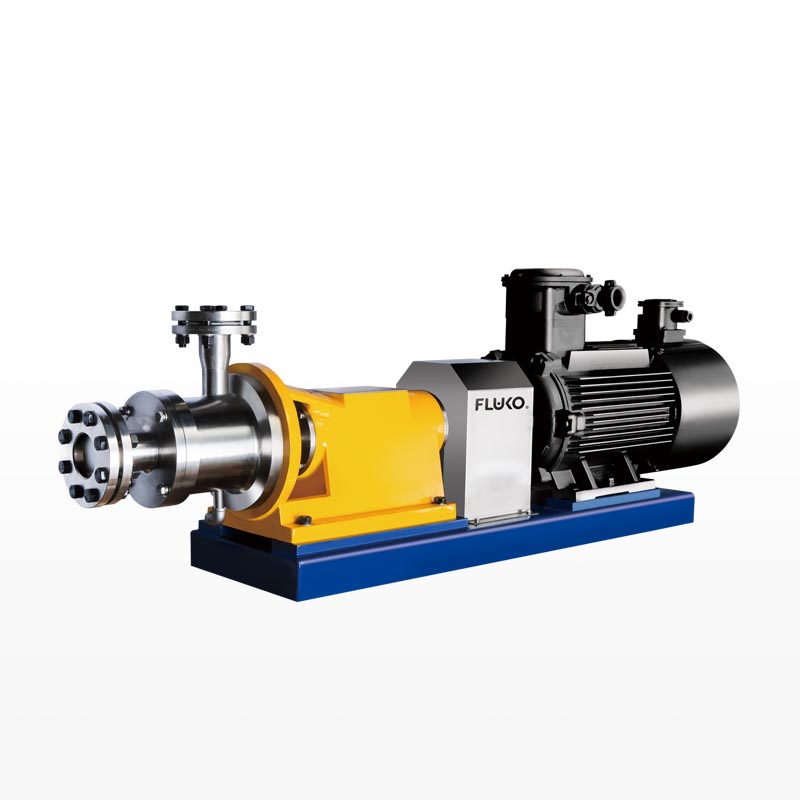
Production lines frequently deliver product variance: inconsistent particle size, unstable emulsions, and batch-to-batch drift that sabotage shelf life and sensory targets. These failures usually trace to mismatched equipment and process conditions rather than raw materials. When an operation expects narrow droplet-size distributions but deploys a mismatched rotor‑stator or underpowered pump, problems compound. A practical step is to inspect the interface between process intent and equipment capability — for example, swapping a generic rotor array for a purpose-built high shear mixer often removes a major source of variability without changing formulation chemistry.
Root causes and technical constraints
The core technical drivers are fluid rheology, energy dissipation per unit volume, and temperature management. High viscosity raises the power required to achieve a target shear; delicate APIs degrade under excessive shear or heat; seals and surface finishes determine contamination risk. Materials and finish matter: AISI 316L wetted surfaces and electropolishing reduce adhesion and simplify CIP cycles. Pumps, drives, and bearing selections set the real uptime ceiling. Treat each factor as a design variable tied to a measurable outcome (droplet size, transmittance, viscosity), not as an aesthetic or checkbox.
Experience, expertise, and authoritative anchor
Decades of plant-level commissioning and scale-up work inform pragmatic choices: match geometry to viscosity, specify cooling sufficient to limit adiabatic temperature rise, and reconcile nominal throughput with dwell time in the shear zone. Field trials conducted at dairy processing plants in Wisconsin demonstrated measurable fat‑globule size reduction and improved cream stability when equipment and process conditions were aligned; those trials used validated sampling and microscopy protocols consistent with industry standards. For operators seeking equipment-level clarity, validated data from a homogenizer machine run provides the necessary traceable metrics to compare rotor-stator, high-pressure, and ultrasonic options under real process loads.
Design and selection guidelines
Start with target specifications: required throughput, target D50 droplet size, maximum allowable temperature rise, and CIP constraints. Select an architecture that meets those specs: rotor‑stator units for moderate to high throughput with lower capital intensity; high‑pressure homogenizers where submicron emulsions are required; ultrasonic systems for batch lab work and specific fine-dispersion tasks. Confirm materials (316L, FDA‑grade gaskets), surface finish (Ra target), and servicing access. Size the drive and pump to maintain required shear at design throughput rather than at a nominal best-case.
Common pitfalls and corrective actions
1) Underspecifying power: undersized motors lead to stalled shear and inconsistent products — specify continuous-duty ratings and thermal protection. 2) Ignoring thermal effects: add heat exchangers or staged processing if the product is heat-sensitive. 3) Overlooking seal and bearing serviceability: design for quick replacement and inventory common spare parts. 4) Poor scale-up logic: don’t assume lab settings scale linearly — preserve specific energy per unit mass when moving to production. Implement routine particle-size distribution checks rather than relying on single-point tests.
Alternatives and comparative insight
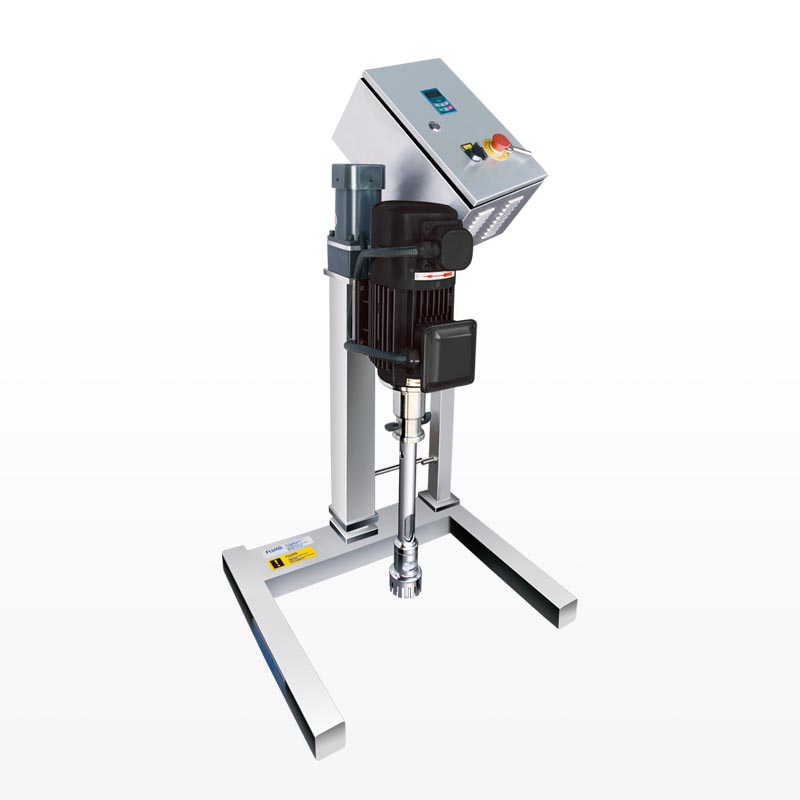
Choose by problem, not brand. When the problem is coarse droplets that destabilize quickly, a high-pressure approach delivers fine, consistent reduction. When the issue is pump shear and solids handling, an industrial rotor‑stator with robust sealing performs better. Ultrasonic systems solve niche degradation and deagglomeration problems but struggle with viscous, particulates-laden streams. Assess total cost of ownership: maintenance intervals, spare parts lead time, and downtime impact on hourly throughput.
Implementation checklist
Define target QC metrics and test methods before procurement. Require factory acceptance tests with representative slurry or emulsion. Include CIP validation and routine maintenance plans in supplier contracts. Train technicians on bearing preload, rotor-stator gap checks, and seal replacement. Capture baseline process-data for the first 100 production hours to spot trends early.
Conclusion
Addressing product inconsistency begins with diagnosing the specific failure mode and matching equipment capability to measurable targets. The right homogenizing approach reduces variability, simplifies quality control, and lowers unplanned downtime when selection follows clear design rules and field-proven practices. Long-term value comes from systems that are serviceable, verifiable, and designed around the formulation and throughput they must deliver; that practical synthesis is exactly what FLUKO brings to production planning and execution.